Choosing reliable China Hrc Slitting Line manufacturers and suppliers requires more than comparing prices. A slitting line may look impressive in a showroom, yet its real value appears during continuous production. Coil width, thickness, tensile strength, line speed, strip accuracy, and recoiler stability all deserve careful review. Small details matter. A poorly aligned knife shaft can create burrs, uneven edges, and costly downtime.
This guide introduces leading Chinese suppliers through practical purchasing criteria. It considers engineering experience, equipment configuration, automation capability, quality control, installation support, and after-sales service. Buyers should request material certificates, machine drawings, trial-cutting videos, and clear performance data. Factory visits can also reveal assembly standards, testing procedures, and spare-parts readiness. Customer references remain useful, although they should be checked independently.
No supplier is perfect. Some manufacturers offer strong mechanical design but limited overseas support. Others provide responsive service but less flexibility for customized coil specifications. This comparison recognizes those differences instead of presenting a single “best” choice. Reliable evaluation depends on matching the supplier’s proven capabilities with the buyer’s actual production needs. Questions about warranty terms, electrical components, safety protection, operator training, and delivery schedules should be answered in writing. With careful verification, purchasers can reduce technical risk and select a Hrc Slitting Line that delivers consistent performance, safer operation, and more predictable long-term costs.
HRC Slitting Lines: Definition, Purpose, and Industrial Applications
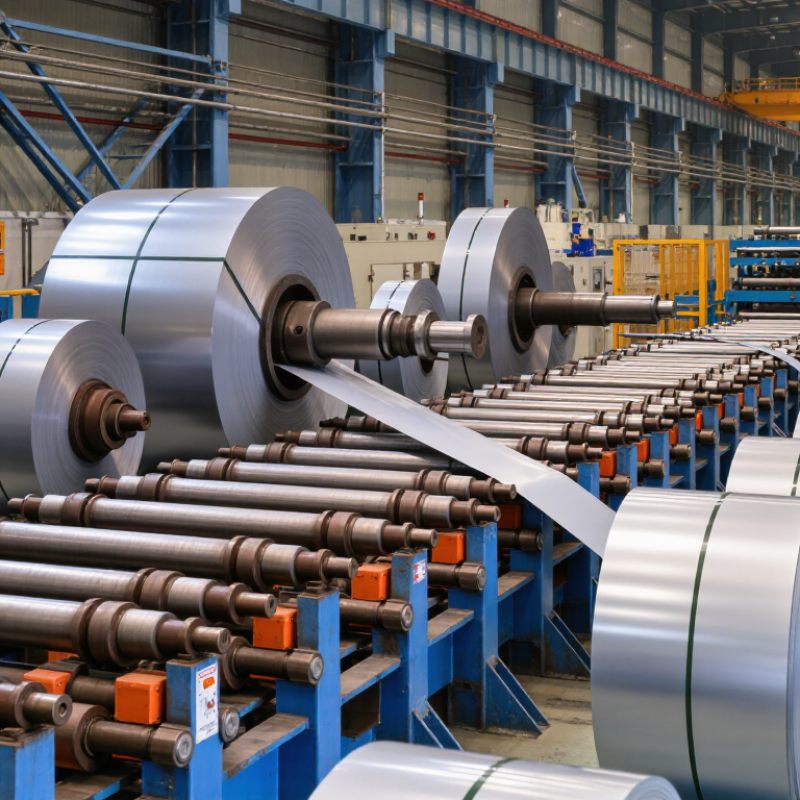
HRC slitting lines process wide hot rolled coils into narrower steel strips. HRC means hot rolled coil, produced through high-temperature rolling. The line typically includes a coil car, uncoiler, leveler, slitting head, separator, and recoiler. Rotary knives cut the moving strip with controlled width accuracy. The recoiler then forms tight, stable coils for later production.
The purpose is practical. It converts large coils into sizes suited to different manufacturing needs. Steel service centers use slit HRC for resale and custom orders. Tube mills turn these strips into welded pipes and structural sections. Construction companies use them for frames, supports, and fabricated components. Automotive and machinery plants may require controlled widths for formed parts. Surface condition, thickness, coil weight, and required tolerance influence the line design.
Chinese manufacturers and suppliers often provide complete engineering, machine testing, installation support, and spare-parts guidance. Experienced buyers should check knife materials, tension control, electrical protection, and documentation. Production samples matter more than attractive specifications. A line may run well during testing but struggle with thin edges or uneven coils. That risk deserves honest discussion. Operators also need training for setup, knife clearance, and safe coil handling. No line is perfect. Regular inspection still prevents avoidable downtime.
HRC slitting lines process hot rolled coils into narrower strips for structural, automotive, and fabrication applications. Reliable equipment should match the coil width, thickness, yield strength, and surface condition. Typical specifications include coil widths from 500 to 2,000 mm, thicknesses from 1.5 to 12 mm, and line speeds of 60 to 120 meters per minute. Actual capacity depends on material grade and strip width.
A strong line uses a rigid entry guide, hydraulic decoiler, precision slitting head, and stable recoiler. Knife diameter, arbor size, spacer accuracy, and clearance control directly affect edge quality. Automatic tension control helps prevent telescoping during recoiling.
A PLC system should monitor speed, torque, strip tracking, and emergency stops. Safety guarding matters too. It is not optional. Experienced suppliers also provide trial slitting, installation support, and operator training. These services often reveal problems that brochures miss.
Tips: Confirm the maximum coil weight, expansion range, and motor torque before choosing equipment. Request sample strips from your own HRC grade. Check burr height, camber, and coil tightness. No line is perfect. Even advanced systems need regular knife inspection, alignment checks, and tension adjustments. A small setup error can create visible edge waves or uneven recoils. Some buyers focus too much on speed, but stable output usually matters more than the highest advertised number.
Evaluating China’s HRC slitting line manufacturers requires more than comparing prices. Start with technical fit. Confirm the incoming hot-rolled coil grade, thickness range, maximum width, coil weight, and required strip width. A line designed for light gauge material may struggle with heavy HRC coils.
Ask for measured performance data, not general promises. Check line speed, slitting accuracy, tension stability, edge condition, and recoiling quality. Request videos from comparable installations. Better still, arrange a factory inspection and witness a material trial using your steel specification.
Review the machine structure carefully. Pay attention to the uncoiler, leveler, slitter head, scrap winder, tension unit, recoiler, and hydraulic systems. Inspect shaft rigidity and tool adjustment methods. Small design weaknesses can create burrs, telescoping coils, or frequent downtime. These details matter.
A reliable supplier should provide drawings, electrical diagrams, operating manuals, inspection records, and a clear spare-parts list. Confirm response times for remote support and the availability of technicians. Customer references should include similar coil sizes and production targets, not only impressive photographs.
I would not trust a polished brochure alone. Some performance figures may reflect ideal conditions. Ask how results change with harder steel, variable coil thickness, or operator mistakes. A factory may also avoid discussing maintenance limits. That silence deserves attention. Compare total ownership cost, including tooling, training, energy use, consumables, and commissioning. A lower purchase price can become expensive when support is slow.
| Evaluation Dimension | Typical HRC Slitting-Line Requirement | Recommended Evaluation Benchmark | Documents or Evidence to Request | Suggested Weight |
|---|---|---|---|---|
| Applicable Material | Hot-rolled carbon steel, weathering steel, structural steel, or other specified grades. | The supplier clearly states compatible steel grades, yield strength, tensile strength, surface condition, and temperature limits. | Material specification sheet, application list, and sample-production records. | 8% |
| Thickness and Strip-Width Range | HRC processing commonly involves heavier gauges and wider coils than cold-rolled applications; the actual range depends on the line design. | Verify the maximum entry thickness, minimum slit width, maximum coil width, number of cuts, and finished-strip tolerance against the buyer’s real coil program. | Guaranteed technical parameters, approved layout, and dimensional tolerance table. | 15% |
| Coil Weight and Mandrel Capacity | Heavy-duty lines require an entry coil car, uncoiler, recoiler, and mandrels designed for the specified coil weight and inside diameter. | Rated capacity should exceed the heaviest planned coil with an appropriate engineering margin; confirm coil ID, OD, and maximum unit weight. | Load calculations, mandrel drawings, hydraulic specifications, and factory acceptance criteria. | 12% |
| Line Speed and Throughput | Operating speed is influenced by thickness, grade, strip width, knife setup, coil weight, and required edge quality. | Compare guaranteed production speed under the buyer’s actual material conditions, not only the no-load maximum speed. | Cycle-time calculation, performance guarantee, speed-versus-thickness chart, and trial results. | 12% |
| Slitting Accuracy and Edge Quality | Key results include strip-width accuracy, burr control, camber, telescoping, and stable separation of slit strands. | Require measurable tolerances defined for the specific thickness and grade; do not accept only general claims such as “high precision.” | Inspection standards, sample strips, measurement reports, and acceptance-test procedures. | 15% |
| Knife and Tooling System | The line should include suitable rotary knives, spacers, separators, tool storage, and a practical setup method for the planned product mix. | Assess knife material, tool-life records, changeover time, spacer accuracy, and availability of replacement tooling. | Tool drawings, hardness or material certificates, setup instructions, and spare-parts quotation. | 10% |
| Automation and Control | A modern line typically uses PLC-based control, variable-frequency or servo drives, tension control, sensors, alarms, and a human-machine interface. | Check recipe management, tension stability, fault diagnostics, data access, cybersecurity expectations, and operator permissions. | Control architecture, I/O list, software backup policy, HMI screenshots, and automation spare-parts list. | 8% |
| Safety and Compliance | The equipment should address guarding, emergency stops, interlocks, safe access, hydraulic risks, electrical protection, and stored-energy hazards. | Evaluate against the regulations applicable at the installation site and require a documented risk assessment before shipment. | Risk assessment, safety-circuit drawings, conformity documentation, manuals, and inspection checklist. | 10% |
| Fabrication and Quality Control | Critical components include frames, shafts, bearings, hydraulic units, gearboxes, electrical cabinets, and precision knife assemblies. | Confirm traceable inspections for machining, welding, alignment, electrical wiring, pressure testing, and final assembly. | Quality plan, inspection and test plan, material certificates, calibration records, and factory test reports. | 8% |
| Installation, Commissioning, and Training | Successful commissioning requires mechanical installation, electrical connection, line alignment, knife setup, trial production, and operator training. | Prefer a supplier offering documented commissioning milestones, multilingual manuals, training hours, and production support. | Installation scope, schedule, training plan, commissioning protocol, and acceptance certificate template. | 5% |
| After-Sales Service and Spare Parts | Long-term availability of bearings, sensors, knives, spacers, seals, drive components, and control-system parts affects uptime. | Assess response time, remote-support capability, service personnel availability, warranty terms, and recommended critical spares. | Warranty policy, service-level agreement, spare-parts price list, response-time commitment, and customer references. | 5% |
| Total Evaluation Weight | Use a weighted scorecard based on the buyer’s actual HRC grades, coil dimensions, output targets, and installation requirements. | A supplier should be shortlisted only after technical compliance, factory verification, and documented performance testing. | Completed technical questionnaire, audit report, FAT record, and signed performance guarantees. | 100% |
Note: The benchmark ranges and evaluation points should be customized to the purchaser’s material grades, coil dimensions, required output, local safety regulations, and final-product tolerances.
Selecting a reliable HRC slitting line supplier in China requires more than a polished catalog. Experienced suppliers show complete process knowledge, from coil loading to recoiling and edge trimming. Their engineers should explain strip width, thickness, yield strength, line speed, and required coil weight in practical terms. A factory visit can reveal more than a sales presentation. Look at it closely. Observe weld quality, machine alignment, guarding, and operating instructions.
Customization should solve a production problem, not add attractive options. Suppliers may adjust entry equipment, tension control, knife arrangements, separator discs, and automation levels. A capable team studies your material grades and target widths before proposing a layout. It should also provide drawings, load calculations, commissioning support, and operator training. Ask for trial-cut records. They expose burrs, camber, telescoping, and inconsistent tension before shipment.
Quality depends on repeatable controls, not one final inspection. Look for documented tolerances, incoming-material checks, calibrated instruments, and traceable component records. A quality plan aligned with ISO 9001 principles can improve consistency. Electrical cabinets should be clearly labeled, while emergency stops and interlocks require functional testing. After installation, useful suppliers measure slit-width accuracy, coil shape, surface protection, and output stability. Still, no line is perfect on its first production day. Installation conditions, operator habits, and steel variation can change results. A supplier willing to review these gaps honestly may be more dependable than one promising flawless performance.
Purchasing an HRC slitting line requires more than comparing advertised speed. World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023, showing the scale of this market. However, coil-processing demand differs by thickness, width, grade, and tolerances. Ask suppliers for verified cutting accuracy, changeover time, line tension control, and power consumption. Request references from plants processing similar HRC grades. A low bid can still be the wrong decision.
Installation planning should begin before shipment. Check foundation drawings, crane access, electrical capacity, ventilation, and operator safety zones. Experienced suppliers should provide layout files, commissioning procedures, and practical training. Installation records matter. They reveal whether alignment was measured or merely assumed. Plan spare knives, bearings, sensors, and hydraulic seals before production starts. Small missing parts can delay an entire line.
Tips:
Use a total-cost worksheet covering freight, installation, tooling, training, energy, and downtime. Plant Engineering’s 2023 maintenance survey reported that 82% of respondents experienced unplanned downtime during the previous three years. That figure deserves attention. Require preventive-maintenance schedules, remote diagnostic support, response-time commitments, and clear warranty exclusions. After-sales service should include troubleshooting videos, inspection checklists, and technician availability. Do not accept vague promises. Get service levels in writing, then test them during commissioning. Mistakes happen, even with careful suppliers; honest reporting and corrective action are more valuable than perfect-looking documents.